
Technical Guides
Troubleshooting Corrugated Board Warping: Causes, Prevention, and Solutions
Complete guide to diagnosing and solving corrugated board warping issues, covering S-warp, twist warp, and diagonal warp with practical solutions.
On this page
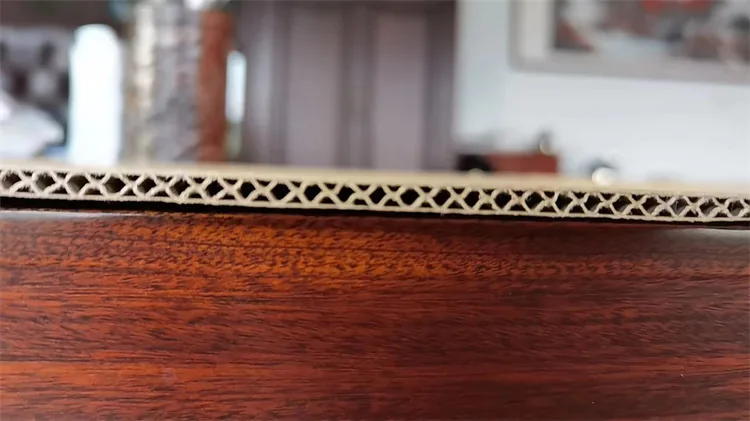
Board warping is one of the most common quality problems in corrugated board production. Understanding the causes and implementing proper controls can significantly reduce warp-related waste and customer complaints.
Types of Warping
- S-Warp (Up-Warp/Down-Warp):
- Board curves along machine direction
- Single-face side curves up (up-warp) or down (down-warp)
- Most common type of warp
- Usually moisture or tension related
- Diagonal Warp (Twist):
- One corner higher than others
- Board twists rather than curves
- Often machine alignment issue
- Can also be caused by uneven tension
- Cross-Direction Warp:
- Board curves across width
- Less common than S-warp
- Usually paper-related
Root Causes of Warping
Moisture Imbalance
- Different moisture content in liner vs. medium
- Different moisture on top vs. bottom liners
- Moisture pickup after production
- Paper storage conditions
Temperature Differences
- Uneven heating at double backer
- One side of board cooling faster
- Ambient conditions at stacker
Tension Imbalance
- Web tension differences between plies
- Uneven brake settings
- Paper roll quality variations
Adhesive Issues
- Over-application causing moisture addition
- Uneven glue lines
- Slow drying on one side
Paper Properties
- Different papers on liner vs. medium
- Paper moisture content from supplier
- Paper curl tendency
- Paper hygro-expansion characteristics
Diagnostic Process
Step 1: Identify Warp Type
- Place board on flat surface
- Measure height of lifted corners/edges
- Note direction of curve
- Check multiple sheets from same run
Step 2: Check Moisture Balance
- Measure moisture content of each ply
- Compare top liner vs. bottom liner
- Check finished board moisture
- Target: All plies within 1-2% of each other
Step 3: Review Process Parameters
- Hot plate temperatures (all zones)
- Web tensions throughout line
- Adhesive application rates
- Line speed vs. dwell time
Step 4: Check Paper Variables
- Paper moisture content as received
- Paper storage conditions
- Paper grade specifications
Solutions by Cause
For Moisture-Related Warp
- Condition papers before use (bring to equilibrium)
- Adjust preheater settings to balance moisture
- Control adhesive application rate
- Ensure adequate drying at double backer
- Control storage humidity
For Temperature-Related Warp
- Balance hot plate temperatures
- Ensure even heating across width
- Allow adequate cooling time before stacking
- Control ambient conditions at stacker
For Tension-Related Warp
- Balance web tension across all plies
- Check and calibrate tension controls
- Verify paper roll quality
- Ensure proper splice tension
Boiler-Free Technology Advantage
Xuegong's flute-to-flute (peak-to-peak) technology specifically addresses warping
- Diamond structure resists warping forces
- Lower operating temperatures = less thermal stress
- More consistent adhesive curing
- Documented reduction in warp-related complaints
The patented flute-to-flute structure creates inherent stability that traditional single-medium boards cannot match. Contact Xuegong for technical consultation on warp reduction strategies.
More in Technical Guides
Honeycomb Facing Glue: Floor Mixing for the Two Routes
Mix honeycomb facing glue on one of two routes. Water only uses 25 kg of powder and 30–40 kg of water. Adding starch uses 25 kg and 40–60 kg, in two tanks. Do not use this sheet on core glue.
Honeycomb Lines: Heat, Press, and the Two Speed Windows
Honeycomb core making is about 10–200 m/min. Face laminating is about 4–30 m/min. Cold press and hot press both exist. A slow start can run with the heater off.
Honeycomb Glue Film and Dry Speed: Slow, Fast, Quick, or Instant
Honeycomb line glue can be specified with an elastic or a rigid film, and with dry speed from slow to instant. On water-only facing glue, less water dries faster. Do not go below 30 kg of water.