
Technical Guides
Fundamentals of Corrugated Box Design
Basic principles for designing corrugated boxes that protect products and optimize costs.
On this page
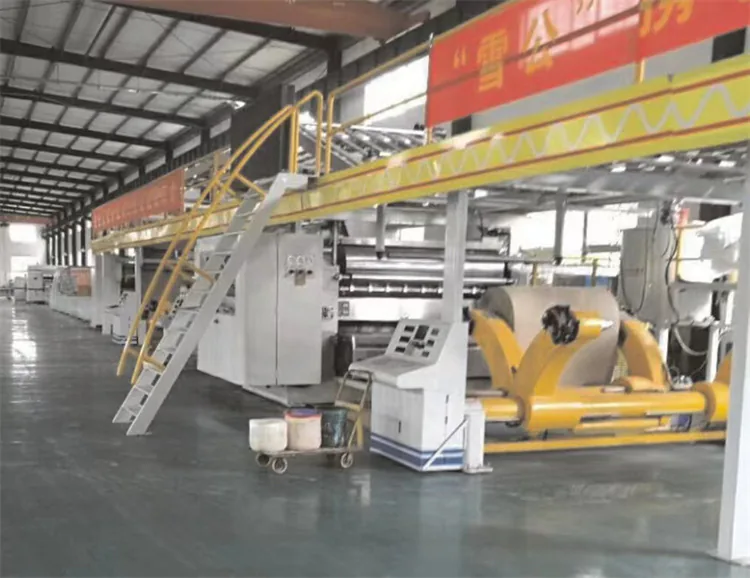
Effective box design balances protection, cost, and functionality. Understanding design fundamentals helps specify the right packaging for each application.
Box Style Terminology
RSC (Regular Slotted Container)
Most common box style. All flaps same length, meeting in center. Efficient and economical.
HSC (Half Slotted Container)
One set of flaps only. Used with separate lid or when bottom must be assembled.
FOL (Full Overlap)
Outer flaps overlap completely. Better stacking strength and protection.
Die-Cut Boxes
Custom shapes cut from flat blanks. Used for retail-ready packaging.
Design Variables
Internal Dimensions
- Length × Width × Height (L×W×H)
- Must accommodate product plus cushioning
- Consider insertion and removal ease
Board Selection
- Single-wall vs double-wall
- Flute profile (A, B, C, E)
- Paper grades and weights
- Based on product weight and fragility
Flap Design
- Standard vs full overlap
- Hand holes and ventilation
- Closure method (tape, glue, staples)
Design Optimization
Right-Sizing
- Minimize void space
- Reduce dimensional weight charges
- Use variable box sizes for product range
Strength Optimization
- Longest dimension as length
- Maximize perimeter for BCT
- Consider print coverage effect
Cost Optimization
- Standard sizes when possible
- Efficient sheet utilization
- Balance protection vs material cost
Testing Requirements
- BCT (Box Compression Test)
- Drop testing
- Vibration testing
- Actual shipping trials
Work with your converter's design team to optimize packaging for your specific products and supply chain.
More in Technical Guides
Honeycomb Facing Glue: Floor Mixing for the Two Routes
Mix honeycomb facing glue on one of two routes. Water only uses 25 kg of powder and 30–40 kg of water. Adding starch uses 25 kg and 40–60 kg, in two tanks. Do not use this sheet on core glue.
Honeycomb Lines: Heat, Press, and the Two Speed Windows
Honeycomb core making is about 10–200 m/min. Face laminating is about 4–30 m/min. Cold press and hot press both exist. A slow start can run with the heater off.
Honeycomb Glue Film and Dry Speed: Slow, Fast, Quick, or Instant
Honeycomb line glue can be specified with an elastic or a rigid film, and with dry speed from slow to instant. On water-only facing glue, less water dries faster. Do not go below 30 kg of water.