
Technical Guides
Understanding Corrugated Board Strength Testing: ECT, BCT, FCT Explained
A practical guide to corrugated board strength testing methods, what the numbers mean, and how to specify the right board for your packaging needs.
On this page
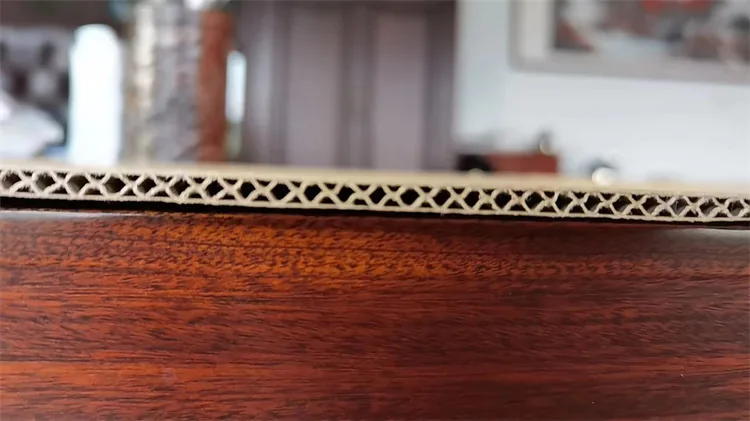
Corrugated board strength is measured through standardized tests that predict real-world performance. Understanding these tests helps you specify the right board for each application and troubleshoot quality issues.
The Three Key Strength Tests
- ECT (Edge Crush Test):
What It Measures: Compressive strength of the board edge—simulates stacking pressure in warehouses.
How It's Done: A small sample (usually 2" × 2") is placed on edge and compressed until failure. Result given in lbs/inch or kN/m.
Why It Matters: ECT directly predicts box stacking strength. Higher ECT = more boxes can be stacked safely.
Typical Values
- Single-wall B-flute: 23-35 ECT
- Single-wall C-flute: 26-44 ECT
- Double-wall BC: 42-82 ECT
- Double-wall AC: 48-112 ECT
- BCT (Box Compression Test):
What It Measures: Total compression strength of a finished box—the actual stacking capacity.
How It's Done: A complete box is placed between platens and compressed until it buckles. Result in lbs or kN.
Why It Matters: BCT is the ultimate measure of box performance. It accounts for box dimensions, not just board strength.
BCT Calculation (McKee Formula)
BCT = 5.87 × ECT × √(Caliper × Perimeter)
Where
- ECT = Edge Crush Test value
- Caliper = Board thickness
- Perimeter = 2 × (Length + Width)
- FCT (Flat Crush Test):
What It Measures: Resistance to crushing force applied perpendicular to the board surface—simulates handling damage.
How It's Done: A sample is placed flat and compressed. Result in lbs/in² or kPa.
Why It Matters: FCT indicates cushioning ability and resistance to impact damage during handling.
Typical Values by Flute
- A-flute: 14-22 psi (best cushioning)
- B-flute: 25-40 psi (good crush resistance)
- C-flute: 18-30 psi (balanced)
- E-flute: 40-60 psi (best surface, least cushioning)
Other Important Tests
Burst Test (Mullen)
- Measures resistance to puncture/rupture
- Legacy specification method (being replaced by ECT)
- Still used in some markets and specifications
Cobb Test
- Measures water absorption of paper surface
- Important for moisture-sensitive products
- Lower Cobb = better water resistance
Pin Adhesion Test
- Measures bond strength between liner and medium
- Indicates adhesive performance
- Important quality control metric
Specifying the Right Board
Step 1: Determine stacking requirements
- How many boxes high?
- Warehouse conditions (humidity, time)?
- Apply safety factor (typically 3:1 to 5:1)
Step 2: Calculate required BCT
Required BCT = (Stack height × Box weight × Safety factor)
Step 3: Select appropriate board grade
- Use McKee formula to find ECT needed
- Choose flute type based on protection vs space
- Specify paper grades to achieve ECT
Adhesive Impact on Strength
Bond quality directly affects board strength. Poor adhesive performance can reduce
- ECT by 10-30% (delamination allows buckling)
- FCT significantly (layers separate under crush)
- Pin adhesion obviously
Use quality adhesive and maintain proper application to achieve specified strength values.
For product matching and trial planning, review /products/board-strengthener and /products/corrugated-board-glue. Xuegong New Materials Group can help align adhesive selection with your line speed, paper mix, and quality targets—contact us for samples or a factory quote.
More in Technical Guides
Honeycomb Facing Glue: Floor Mixing for the Two Routes
Mix honeycomb facing glue on one of two routes. Water only uses 25 kg of powder and 30–40 kg of water. Adding starch uses 25 kg and 40–60 kg, in two tanks. Do not use this sheet on core glue.
Honeycomb Lines: Heat, Press, and the Two Speed Windows
Honeycomb core making is about 10–200 m/min. Face laminating is about 4–30 m/min. Cold press and hot press both exist. A slow start can run with the heater off.
Honeycomb Glue Film and Dry Speed: Slow, Fast, Quick, or Instant
Honeycomb line glue can be specified with an elastic or a rigid film, and with dry speed from slow to instant. On water-only facing glue, less water dries faster. Do not go below 30 kg of water.