
Technical Guides
Preventing Corrugated Board Delamination
Understanding why corrugated board layers separate and how to ensure strong, lasting bonds.
On this page
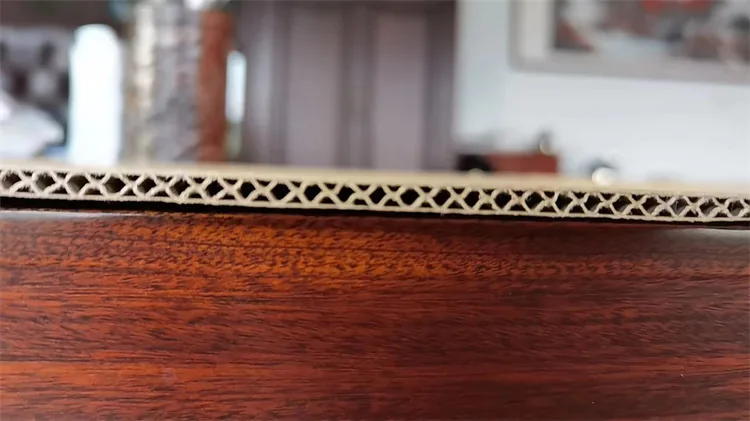
Delamination—separation of the liner from the fluted medium—is one of the most serious quality defects in corrugated board. It compromises box strength and can lead to customer complaints and returns.
Types of Delamination
Single Facer Delamination: Liner separates from medium immediately after the single facer. Usually visible as bubbles or loose areas.
Double Backer Delamination: Bond failure between single-face web and liner at the double backer. May not appear until cutting or handling.
Delayed Delamination: Board appears good initially but delaminates during storage or use. Often caused by moisture-related stress.
Common Causes
Adhesive Issues
- Insufficient adhesive application
- Adhesive viscosity too high (poor penetration)
- Adhesive temperature incorrect
- Gel temperature too high or too low
- Contaminated or old adhesive
Process Issues
- Insufficient pressure at bond point
- Line speed too fast for adhesive to set
- Inadequate heat for gelatinization
- Poor paper-to-roll contact
Paper Issues
- Paper surface treatments repelling adhesive
- High-ash recycled papers with poor bonding
- Excessive moisture in paper rolls
Diagnostic Approach
- Identify where delamination is occurring (SF or DB)
- Check adhesive application uniformly across web
- Verify adhesive preparation (viscosity, temperature)
- Test paper for surface treatments or contamination
- Review recent process or material changes
Solutions
- Optimize adhesive viscosity for paper type
- Ensure proper gel temperature (58-62°C typical)
- Adjust pressure and gap settings
- Consider switching to instant-setting adhesive
- Work with paper supplier on bonding issues
More in Technical Guides
Honeycomb Facing Glue: Floor Mixing for the Two Routes
Mix honeycomb facing glue on one of two routes. Water only uses 25 kg of powder and 30–40 kg of water. Adding starch uses 25 kg and 40–60 kg, in two tanks. Do not use this sheet on core glue.
Honeycomb Lines: Heat, Press, and the Two Speed Windows
Honeycomb core making is about 10–200 m/min. Face laminating is about 4–30 m/min. Cold press and hot press both exist. A slow start can run with the heater off.
Honeycomb Glue Film and Dry Speed: Slow, Fast, Quick, or Instant
Honeycomb line glue can be specified with an elastic or a rigid film, and with dry speed from slow to instant. On water-only facing glue, less water dries faster. Do not go below 30 kg of water.