
Technical Guides
Preventing and Fixing Corrugated Board Warping
Understanding the causes of board warp and practical solutions for producing flat corrugated board.
On this page
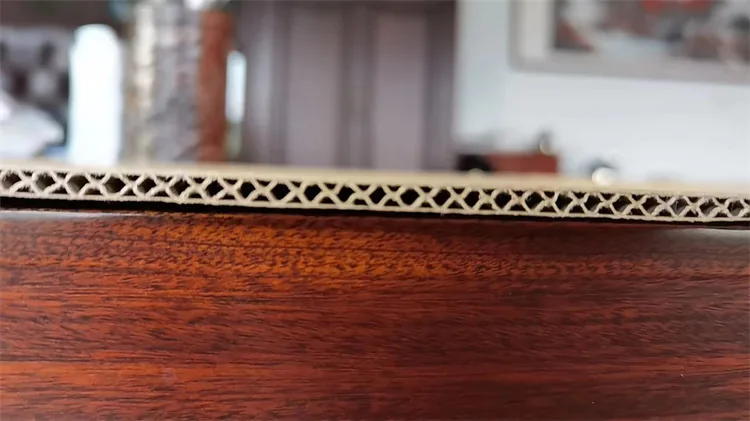
Warped corrugated board is one of the most common quality problems, affecting downstream conversion and customer satisfaction. Understanding warp causes leads to effective solutions.
Types of Warp
S-Warp (Diagonal)
Board curves diagonally from corner to corner. Usually caused by uneven moisture or tension across the web.
Cross-Machine Warp
Edges curl up or down relative to center. Caused by moisture differences between edges and center.
Machine-Direction Warp
Board curves along its length. Often caused by tension or moisture differences between liner and medium.
Twist
Combination of warps creating a twisted board. Most complex to diagnose and fix.
Root Causes
Moisture Imbalance
- Liner and medium with different moisture content
- Uneven drying across web width
- Paper absorbing moisture from adhesive
- Environmental humidity changes
Tension Imbalance
- Different tension on top and bottom liners
- Web tracking issues
- Uneven roll hardness
Adhesive Issues
- Excessive adhesive application
- Uneven glue distribution
- Adhesive penetration differences
Prevention Strategies
Paper Management
- Match moisture content of all papers
- Acclimate paper before use
- Store properly to prevent moisture pickup
Process Control
- Balance web tensions
- Ensure even adhesive application
- Monitor moisture across web width
- Use moisture control systems
Adhesive Selection
- Use instant-setting adhesive to minimize moisture addition
- Ensure proper viscosity for paper type
- Optimize application weight
Corrective Actions
- Identify which layer is causing warp
- Adjust preheating/conditioning
- Rebalance tensions
- Consider adhesive formula change
More in Technical Guides
Honeycomb Facing Glue: Floor Mixing for the Two Routes
Mix honeycomb facing glue on one of two routes. Water only uses 25 kg of powder and 30–40 kg of water. Adding starch uses 25 kg and 40–60 kg, in two tanks. Do not use this sheet on core glue.
Honeycomb Lines: Heat, Press, and the Two Speed Windows
Honeycomb core making is about 10–200 m/min. Face laminating is about 4–30 m/min. Cold press and hot press both exist. A slow start can run with the heater off.
Honeycomb Glue Film and Dry Speed: Slow, Fast, Quick, or Instant
Honeycomb line glue can be specified with an elastic or a rigid film, and with dry speed from slow to instant. On water-only facing glue, less water dries faster. Do not go below 30 kg of water.