
Technical Guides
How to Fix Wash Boarding Defects in Corrugated Board
Identifying causes and solutions for the wash boarding effect that creates visible flute patterns on liner surfaces.
On this page
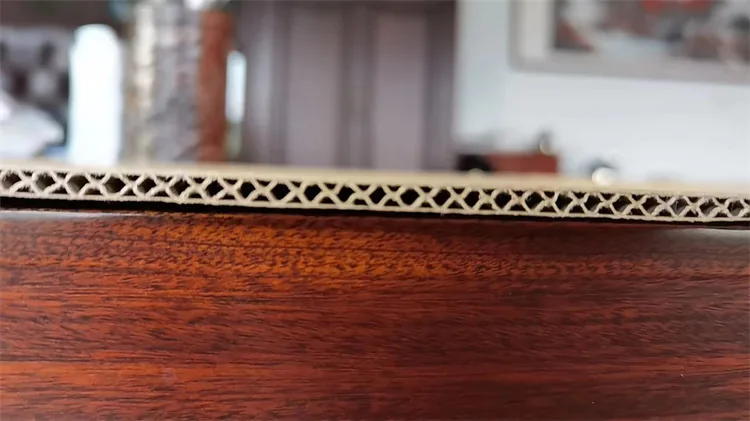
Wash boarding—also called corrugator shadow or flute show-through—occurs when the flute pattern becomes visible on the outer liner surface. This defect affects print quality and product appearance.
What Causes Wash Boarding
- Excessive Adhesive Application:
Too much adhesive creates wet spots that swell the liner unevenly over the flute tips, causing the pattern to show through.
- Excessive Pressure:
Over-pressure at the double backer crushes the board, making flute tips more visible.
- Moisture Imbalance:
When the liner has different moisture content than the medium, it can shrink or expand unevenly.
- Thin or Low-Quality Liner:
Lightweight liners show flute patterns more readily than heavier papers.
- High Hot Plate Temperature:
Excessive heat can cause rapid, uneven drying that accentuates the flute pattern.
Solutions and Adjustments
Adhesive Optimization
- Reduce glue application weight
- Ensure uniform glue film across the web
- Check doctor roll gaps and condition
- Use instant-setting adhesive to minimize moisture penetration
Process Adjustments
- Reduce double backer pressure
- Lower hot plate temperature gradually
- Balance moisture between liner and medium
- Check and adjust wrap angles
Paper Selection
- Use heavier liner basis weights
- Choose papers with good opacity
- Consider surface-treated liners for critical applications
Quality Verification
Inspect board at multiple points along the web to identify where the defect originates. This helps target corrective actions effectively.
More in Technical Guides
Honeycomb Facing Glue: Floor Mixing for the Two Routes
Mix honeycomb facing glue on one of two routes. Water only uses 25 kg of powder and 30–40 kg of water. Adding starch uses 25 kg and 40–60 kg, in two tanks. Do not use this sheet on core glue.
Honeycomb Lines: Heat, Press, and the Two Speed Windows
Honeycomb core making is about 10–200 m/min. Face laminating is about 4–30 m/min. Cold press and hot press both exist. A slow start can run with the heater off.
Honeycomb Glue Film and Dry Speed: Slow, Fast, Quick, or Instant
Honeycomb line glue can be specified with an elastic or a rigid film, and with dry speed from slow to instant. On water-only facing glue, less water dries faster. Do not go below 30 kg of water.