
Technical Guides
How to Solve High-Low Flute Issues on Single Facers
Guidance on managing moisture levels and paper condition to eliminate flute defects.
troubleshootingquality controlsingle facer
On this page
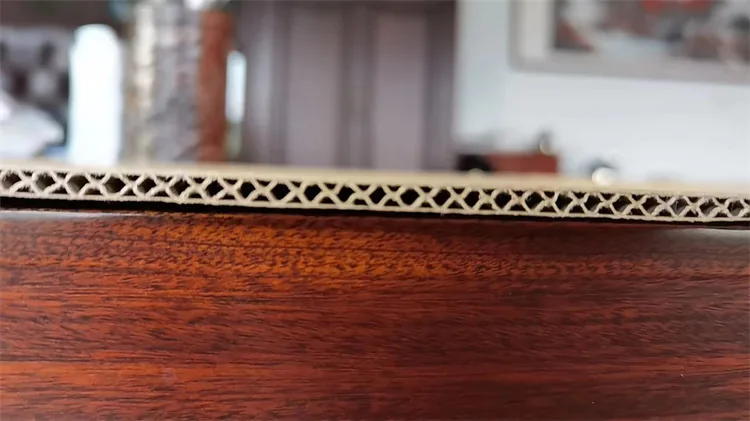
High-low flute defects occur when flute peaks are not uniform in height.
Primary Causes
- Uneven Moisture Content in corrugating medium
- Damaged or improperly stored paper rolls
- Worn or damaged corrugating rolls
Solutions
- Maintain storage at 20-25°C, 50-60% RH
- Allow 24-hour acclimation before use
- Regular roll inspection and maintenance
More in Technical Guides
Honeycomb Facing Glue: Floor Mixing for the Two Routes
Mix honeycomb facing glue on one of two routes. Water only uses 25 kg of powder and 30–40 kg of water. Adding starch uses 25 kg and 40–60 kg, in two tanks. Do not use this sheet on core glue.
Honeycomb Lines: Heat, Press, and the Two Speed Windows
Honeycomb core making is about 10–200 m/min. Face laminating is about 4–30 m/min. Cold press and hot press both exist. A slow start can run with the heater off.
Honeycomb Glue Film and Dry Speed: Slow, Fast, Quick, or Instant
Honeycomb line glue can be specified with an elastic or a rigid film, and with dry speed from slow to instant. On water-only facing glue, less water dries faster. Do not go below 30 kg of water.