
Technical Guides
Corrugated Packaging Glossary: 50 Essential Terms
A comprehensive glossary of technical terms used in corrugated board production and packaging.
On this page
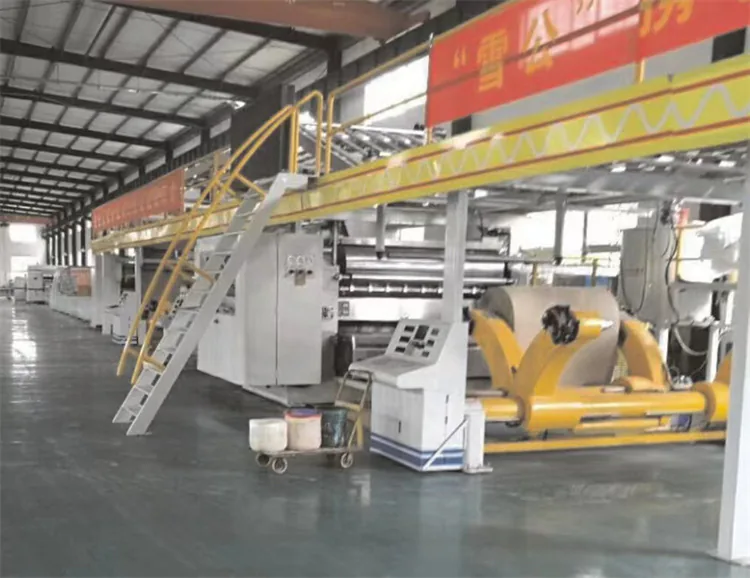
Understanding industry terminology is essential for effective communication with suppliers, customers, and equipment manufacturers. Here are 50 key terms.
Board Components
- Liner: The flat facing sheets on the outside of corrugated board
- Medium (Fluting): The wavy corrugated paper between liners
- Single-Face: One liner glued to corrugated medium
- Single-Wall: Fluted medium between two liners (3-ply)
- Double-Wall: Two mediums with three liners (5 or 7-ply)
Flute Types
- A-Flute: Largest flute, ~4.8mm, excellent cushioning
- B-Flute: ~3.0mm, good crush resistance
- C-Flute: ~4.0mm, most common profile
- E-Flute: ~1.5mm, excellent print surface
- F-Flute: ~0.8mm, thinnest standard flute
Production Equipment
- Single Facer: Makes single-face corrugated
- Double Backer: Bonds liner to single-face web
- Bridge: Accumulates single-face web between stations
- Hot Plates: Heat the board during double backer bonding
- Slitter-Scorer: Cuts and scores board to width
- Cut-Off: Cuts board to length
Quality Measurements
- ECT (Edge Crush Test): Measures stacking strength
- FCT (Flat Crush Test): Measures cushioning
- BCT (Box Compression Test): Measures box strength
- Cobb Test: Measures water absorption
- Caliper: Board thickness
Adhesive Terms
- Gel Temperature: Temperature at which starch gelatinizes
- Viscosity: Adhesive flow resistance (Stein-Hall seconds)
- Carrier: Pre-cooked starch that suspends raw starch
- Tack: Adhesive stickiness
- Open Time: Time adhesive remains workable
Production Terms
- MSF: Thousand Square Feet (production unit)
- Web: Continuous sheet of paper or board
- Warp: Board curling or twisting
- Wash Boarding: Visible flute pattern on liner
- Delamination: Separation of board layers
This glossary covers English terms commonly used internationally. Local markets may use different terminology.
More in Technical Guides
Honeycomb Facing Glue: Floor Mixing for the Two Routes
Mix honeycomb facing glue on one of two routes. Water only uses 25 kg of powder and 30–40 kg of water. Adding starch uses 25 kg and 40–60 kg, in two tanks. Do not use this sheet on core glue.
Honeycomb Lines: Heat, Press, and the Two Speed Windows
Honeycomb core making is about 10–200 m/min. Face laminating is about 4–30 m/min. Cold press and hot press both exist. A slow start can run with the heater off.
Honeycomb Glue Film and Dry Speed: Slow, Fast, Quick, or Instant
Honeycomb line glue can be specified with an elastic or a rigid film, and with dry speed from slow to instant. On water-only facing glue, less water dries faster. Do not go below 30 kg of water.